


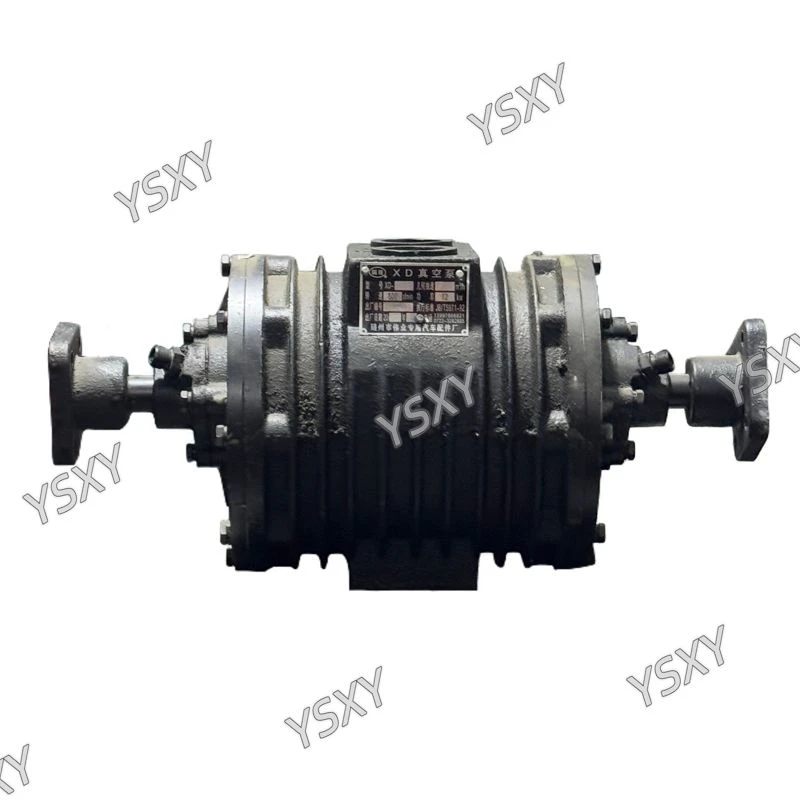


What is a Vacuum Pump?
The vacuum pump is the core component of sewer cleaner trucks, responsible for generating the powerful suction required to extract liquid waste, sludge, and other materials from septic tanks, sewer lines, and industrial sumps-its reliable performance directly dictates the efficiency of waste collection operations. As a specialist in providing high-performance solutions for sanitation equipment, Xi'an Yuesheng Xingyao Trading Co., Ltd. offers premium Vacuum Pumps specifically engineered for sewer cleaner trucks and vacuum tankers. Through strategic collaboration with certified manufacturers, we ensure each vacuum pump delivers exceptional suction power, consistent reliable operation, and an extended service life even in the most demanding waste management scenarios. Built with robust construction and advanced sealing technology, our vacuum pumps stand as the ideal choice for efficient sewage and sludge extraction in municipal sanitation operations, perfectly complementing the component's core functionality to optimize operational productivity and durability in critical waste handling applications.
Product Specifications
|
Parameter |
Value/Description |
|
Pump Type |
Disc rotary vacuum pump, Liquid ring vacuum pump |
|
Displacement |
300-1200 m³/h |
|
Ultimate Vacuum |
≤ -95 kPa |
|
Operating Speed |
1000-3000 rpm |
|
Drive Type |
Belt drive, Direct drive |
|
Shaft Power |
15-75 kW |
|
Material Construction |
Cast iron pump body, stainless steel parts |
|
ealing System |
Mechanical seal, Oil seal |
|
Lubrication |
Forced lubrication, Oil bath lubrication |
|
Protection Level |
IP55, Corrosion-resistant |
Product Features
Powerful Suction Performance: Delivers high vacuum levels for efficient waste extraction in various conditions.
Robust Construction: Heavy-duty cast iron construction withstands the rigors of continuous sanitation operations.
Corrosion Resistance: Special coatings and material selections protect against corrosive waste liquids and chemicals.
Low Maintenance Design: Easy-access components and simple maintenance procedures reduce service downtime.
Thermal Stability: Efficient cooling system maintains optimal operating temperatures during extended use.
Anti-Clogging Design: Optimized internal passages prevent clogging from debris and solid particles.
Energy Efficient: Advanced design minimizes power consumption while maintaining high performance.
Precision Rotors: Balanced rotors with special surface treatment for smooth operation and long life.
Advanced Sealing: Multiple sealing points with high-quality seals prevent leakage and maintain vacuum.
Efficient Cooling: Optimized cooling system with large heat dissipation surfaces.
Easy Maintenance: Modular design with accessible service points for quick maintenance.
Vibration Damping: Built-in vibration dampeners reduce noise and extend component life.
Product Applications
Sewer Cleaner Trucks
Vacuum Tanker Trucks
Septic Tank Pump Trucks
Industrial Waste Collection Vehicles
Municipal Sludge Transport Trucks
Hazardous Liquid Handling Vehicles
Product Certifications & Evidence
Our Vacuum Pumps for sewer cleaner trucks meet stringent quality and performance standards:
ISO 9001:2015 Certified: Quality management system certification.
Performance Testing: Rigorous testing including vacuum performance, endurance, and leakage tests.
Material Certification: Certified materials with traceable origins and quality reports.
Durability Validation: Extended life testing under simulated operational conditions.
Safety Compliance: Meets relevant mechanical and electrical safety standards.
Quality Assurance: Comprehensive inspection of all critical components and assemblies.
Considerate Services
We provide comprehensive support for sanitation vehicle operations:
Pre-Sales: Technical consultation for pump selection based on vehicle specifications and operational requirements.
In-Sales: Flexible order options with reliable delivery to support fleet maintenance schedules.
After-Sales: Installation guidance, operational training, maintenance support, and readily available spare parts.
FAQ
Q: What is the typical maintenance interval for these vacuum pumps?
A: Recommended maintenance intervals are every 500 operating hours for routine service, with major inspection every 2000 hours.
Q: Can the pump handle abrasive materials in sewage?
A: Yes, our pumps are designed with wear-resistant materials to handle abrasive particles commonly found in sewage and sludge.
Q: What is the expected service life in severe operating conditions?
A: With proper maintenance, typical service life is 3-5 years in severe sanitation applications.
Q: How do I determine the correct pump size for my sewer cleaner truck?
A: Please provide your tank capacity, required evacuation time, and typical material viscosity for proper pump selection.
Q: Are spare parts readily available?
A: Yes, we maintain adequate inventory of common spare parts including seals, vanes, and bearings for quick shipment.
Hot Tags: vacuum pump, China vacuum pump manufacturers, suppliers, factory


